
 2024-11-01
 PODCAST
 share
A vegetable line is running, but the incoming crop changes through the shift. Should you alter belt speed, cooling conditions or the load entering the freezer? Food freezing optimisation starts by connecting those choices to product measurements. A digital model can help compare settings when its predictions hold up against the real process.
What food freezing optimisation needs to measure
Freezing removes heat from food and turns part of its water into ice. Rapid freezing generally forms smaller crystals and helps limit damage to texture. Clarence Birdseye helped bring this principle into commercial practice. His double-plate machine followed in 1926, according to the National Inventors Hall of Fame.
For a modern line, the practical question is how quickly the centre of the product reaches the required temperature. Air temperature alone cannot answer it. Product size, starting temperature, composition and loading all affect heat removal.
Individual quick freezing, or IQF, keeps pieces separate. Fluidised beds can achieve this with moving cold air. Plate freezers transfer heat through metal surfaces. The FAO freezing guide explains why equipment choice depends on the product and the process.
Why preparation changes the freezing load
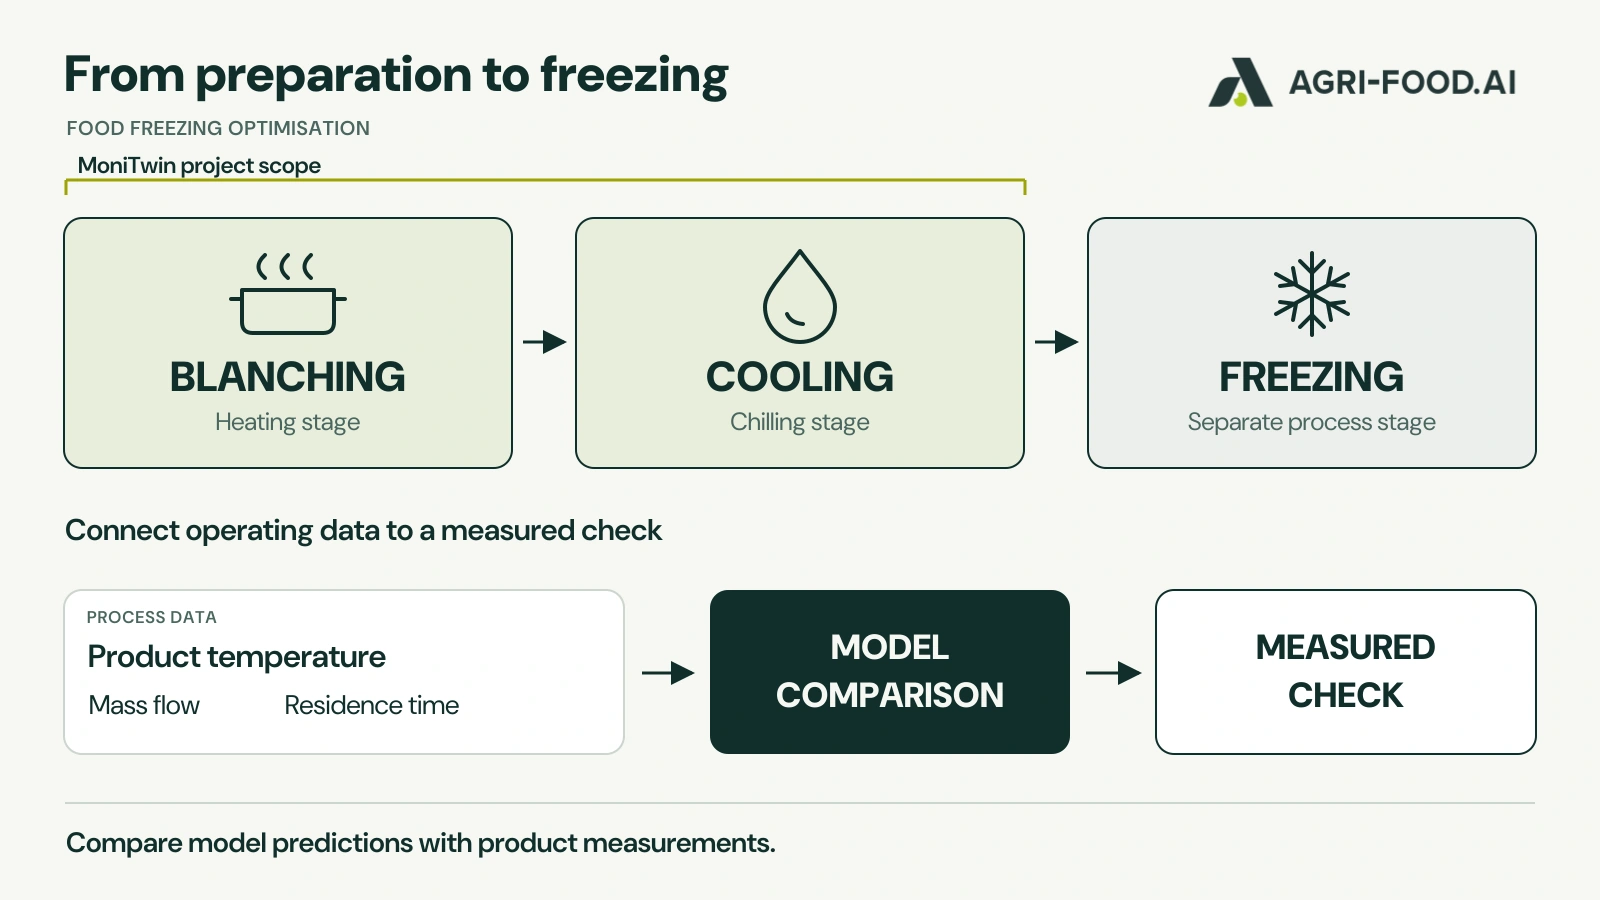
Many vegetables need blanching to limit enzyme activity before freezing. The line then cools the product. These steps affect quality and the heat the freezer must remove. Record the heating and cooling stages separately so a change upstream remains visible downstream.
Begin with product identity, piece size and measured inlet temperature. Add mass flow, residence time and the operating conditions of each stage. Synchronise timestamps and record sensor locations. A probe in the air measures different conditions from one in the food.
For food freezing optimisation, use these records to explain changes between runs. Check calibration and missing readings before treating a sudden change as a process problem. A useful model needs a defined operating range and measurements that represent the product.
Where the Mirelite Mirsa project fits
MoniTwin is AGRI-FOOD.AI’s digital twin solution for vegetable blanching. In this setting, a digital twin connects a process model with operating data to compare how changes may affect production.
The Change2Twin project account, published in July 2024, describes a blanching application at Mirelite Mirsa in Hungary. It links vegetable heating and chilling with mass flow before freezing. The account reports resource benefits without a quantified comparison. This supports a specific application in preparation and cooling, with further work needed to establish performance elsewhere.
Freezing models also have a research basis. Bassani and colleagues in 2021 checked a mathematical freezing model against experimental data for beef and strawberry pulp, then simulated spinach cubes. Their study supports testing heat-transfer predictions against measurements. It provides a separate research example for a different model and set of products.
Test food freezing optimisation on a comparable run
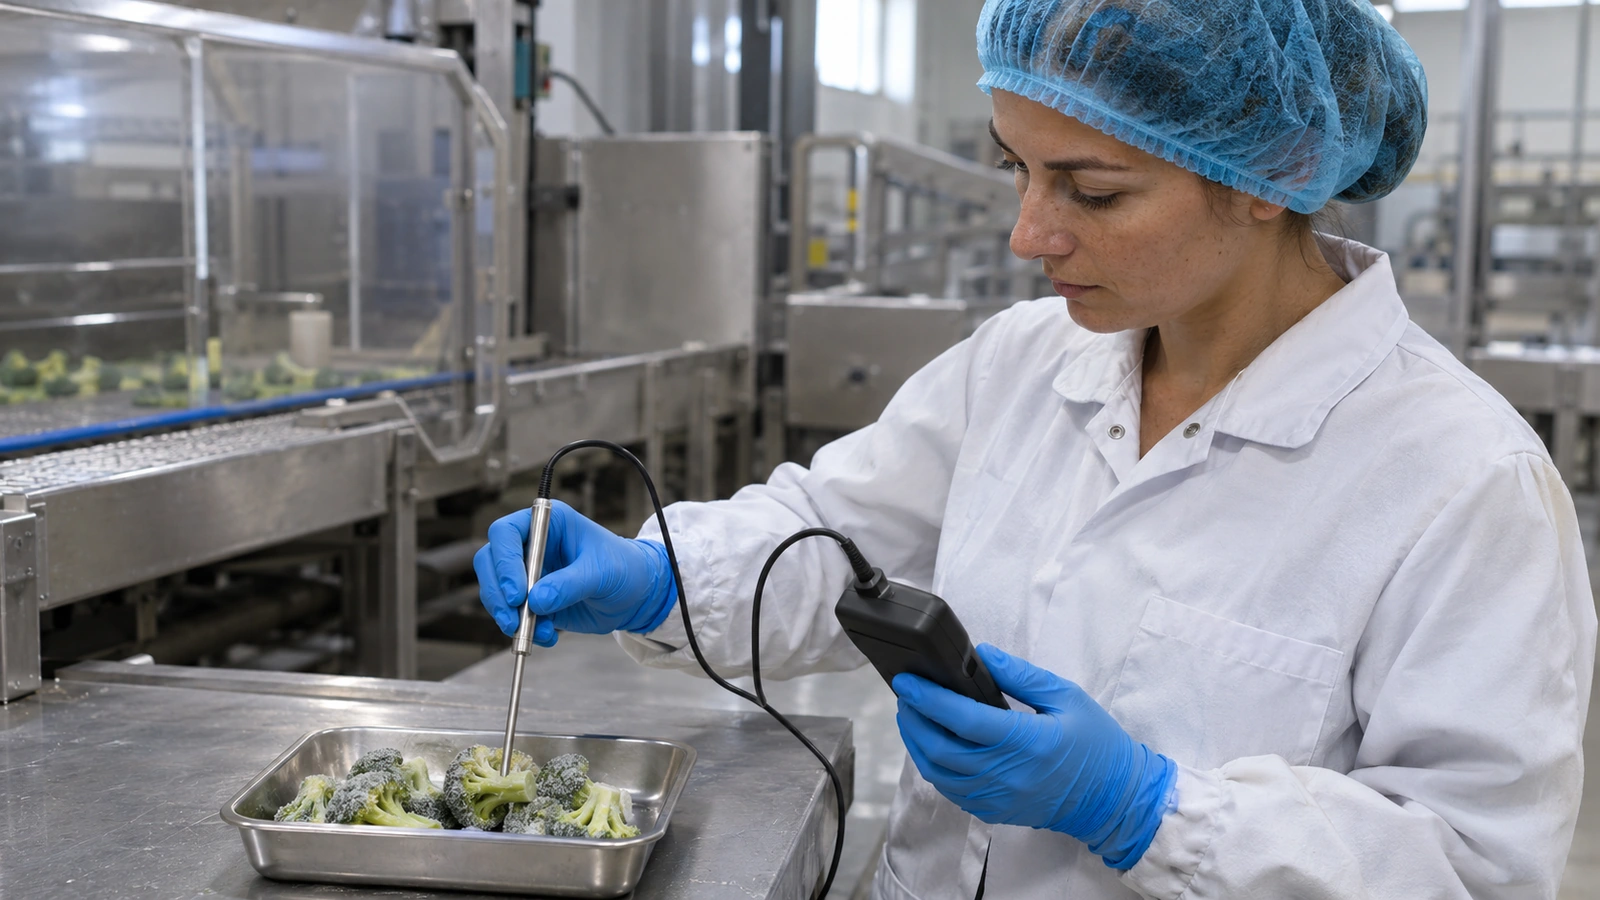
Choose one product and a narrow question, such as whether a different cooling setting changes the heat entering the freezer. Keep the comparison conditions clear and check the outcome with your quality team.
- Record the baseline with product temperature, mass flow and residence time.
- Test one change within the agreed process limits and retain the original settings.
- Compare product quality and energy per kilogram across equivalent measurement periods.
Include the same equipment in both energy measurements and record interruptions, defrost periods and rejected product. A lower electricity reading needs context if throughput or quality also changes.
The original Digital Food Production podcast remains available. Listen to the freezing and digital production episode for the wider discussion.
To discuss food freezing optimisation for your line, send AGRI-FOOD.AI your process stages, available logs and the quality or energy question you want to investigate.
2024-11-01


 Our website uses cookies